

 Reichelt Chemietechnik Magazine
Plastic films have become indispensable in many industrial and laboratory environments. They are used every day for a wide range of purposes. Various manufacturing processes help achieve the required film properties. The main processes for producing plastic films include blown film extrusion and cast film extrusion. This article examines the different manufacturing processes and the specific properties of blown and cast films. It also compares the advantages and disadvantages of each film type.
Uses of Plastic Films in Industry and the Laboratory
Plastic films play an important role in many areas of the laboratory and the processing industry. Their most obvious use is as protective and packaging material for food, chemicals and medical products. However, their specific properties also make them well suited to numerous technical applications, through to specialised laboratory solutions. In the laboratory, they are often used as barrier films, for sealing purposes or to manufacture laboratory equipment. Their versatile characteristics, such as high flexibility, chemical resistance and transparency, make them suitable for many applications.
Blown Film and Cast Film: The Differences
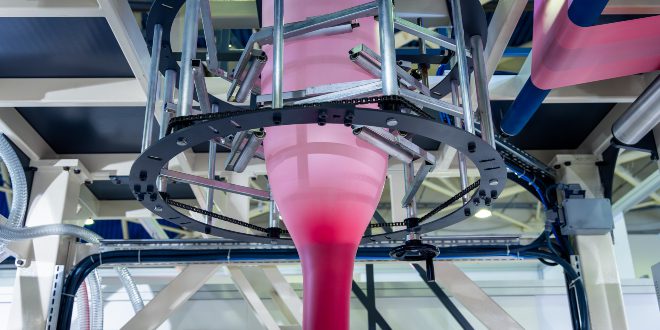
Blown films are produced by inflating an extruded plastic tube. This results in an even wall thickness distribution and good shrink properties.
Cast films, by contrast, are produced by cooling molten plastic that is cast onto a chilled roll. As a result, cast films have a smooth surface. Their thickness can also be set more precisely during the process than that of blown films.
Blown Film Extrusion – Working Principle and Extrusion Line Design
Blown films are made from thermoplastics on a dedicated blown film line. This process is one of the oldest methods of film production.
This creates a film bubble up to 20 m high. Once the tube has solidified, a pair of nip rolls collapses it. The flattened tube then travels to a winder and is wound onto roll cores. Water-cooled processes achieve very high cooling rates. This makes it possible to produce soft, elastic films with an almost amorphous structure.
Basic Layout of a Blown Film Extrusion Line
One of the most important components of a blown film extrusion line is the extruder. It conveys the plastic granulate and, further downstream, the plastic melt. Frictional heat from the screw and the heated barrel zones melt the plastic, which is homogenised in the process. As the material moves forward, the necessary pressure builds up and finally forces the melt through the narrow die gap.
The actual film extrusion follows the extruder. Here, the molten plastic is forced through a die with an annular gap. This forms a tubular structure that is inflated with air. At the same time, air cools the tube externally and, in some applications, internally as well. This stage of the process determines the width and thickness of the film. A key setting for the film’s later properties is the blow-up ratio, which defines how far the tube is inflated.
Once it has cooled completely, the tube is laid flat by nip rolls and then wound up automatically. A single die head can produce films with up to 18 layers in this way.
Types of Blown Film
- Tubular film: The flattened, deflated blown film is usually wound onto cardboard cores. A typical application is the production of plastic sacks.
- Half tubing: A longitudinal slit opens the tube along one edge. The film can then be used for carrier bags with a seamless bottom, for example.
- Single-web film: Slitting both folds of a tubular film produces single-web foil, which can be used as packaging film.
Cast Film Extrusion – Working Principle and Extrusion Line Design
Unlike blown film extrusion, cast film extrusion involves casting the molten plastic onto a chilled roll. There it cools evenly and solidifies. This process allows precise control of film thickness and produces very smooth surfaces.
Basic Layout of a Cast Film Extrusion Line
The melt is cast directly onto a chilled roll, which cools and smooths the material evenly. This produces a very precise thickness and a uniform, smooth surface. After cooling, the film passes over several rolls before it is further processed or wound up.
Calendering is another process that uses rolls to produce plastic films. Cast film extrusion mostly produces thin films. Calendering, however, is better suited to thicker or specially textured films.
Calendering is mainly used for polyvinyl chloride (PVC), which is easy to form. Calendered plastic sheets made of styrene-butadiene-based high-impact polystyrene, on the other hand, are very tough and impact-resistant.
Types of Cast Film
- Monolayer film: A single pass produces a smooth, uniformly formed film for technical applications and packaging, among other uses.
- Multilayer film: Coextrusion makes it possible to form several layers. These give the film additional properties such as barrier functions or extra stability.
Similarities and Differences Between Blown and Cast Films
Both processes can produce films for many different applications. Coextrusion in particular broadens the range of possible variants for both methods. Multilayer plastic films combine the beneficial properties of different plastics in a single film. One laboratory example is the packaging of sterile medical instruments and laboratory samples.
Such packaging often consists of several layers, each with a specific function:
- Outer layer: Robust polyethylene (PE) film that makes the packaging stable and resistant to mechanical stress.
- Tie layer: Bonding layer between the functional layers.
- Barrier layer: For example, a film made of polyamide (PA) or a laminated aluminium foil that forms a barrier against moisture, oxygen and microorganisms.
- Additional tie layer
- Inner layer: Sterilisable and biocompatible layer that keeps the contents free from contamination and allows the pack to be opened safely under sterile conditions.
With this layer structure, sensitive medical devices or laboratory samples stay sterile. They remain protected from external influences such as moisture, oxygen and microorganisms. Both blown and cast films are suitable for this type of packaging. The choice depends on the specific requirements for thickness, surface and barrier properties.
Technical Characteristics of the Film Types at a Glance
| Blown film | Cast film | |
| Thickness distribution | even, but less precise | very precise and even |
| Surface quality | less smooth, often tacky | very smooth |
| Tensile strength | very high | lower |
| Transparency | lower | high transparency possible |
| Flexibility | high | lower |
| Tear propagation resistance | balanced in machine and transverse directions | lower tear propagation resistance |
| Material consumption | efficient use of material | higher material requirement |
| Cost | more economical manufacturing process | more expensive, as production requires greater precision |
| Applications | packaging, bin bags, shrink films, agricultural films | technical films, speciality packaging, precision films, hygiene films |
The comparison shows that each film type has its own specific fields of application. Blown films suit applications that require high tensile strength and flexibility. Cast films serve other purposes thanks to their smooth surface, higher stiffness and precisely adjustable thickness. In both processes, combining several layers into multilayer films creates highly customised structures that unite various beneficial properties.
Image credits:
Featured image | © hodim – stock.adobe.com
Blown film extrusion of a PLA blend| © Kesselring, FKuR Willich, CC BY-SA 3.0 DE <https://creativecommons.org/licenses/by-sa/3.0/de/deed.en>, via Wikimedia Commons
Winding a polyethylene film | © hodim – stock.adobe.com
