 Reichelt Chemietechnik Magazine
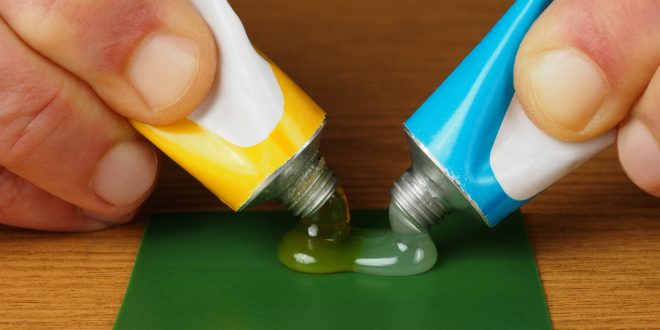
Alongside welding, bolting and soldering, adhesive bonding has become one of the most important techniques for joining metals. Engineering and manufacturing already bond 50 % of all components with adhesives. The automotive industry relies most heavily on adhesive bonding. Aerospace, rail and shipbuilding also use it to join components made of pure aluminium, aluminium-magnesium alloys or steels. Two-component adhesives have long proven themselves here, especially those based on epoxy resins. These epoxy adhesives are known as structural adhesives. But what do plastic adhesives need to bond plastics and other materials durably and withstand environmental stresses?
Why Plastics Need Special Adhesives
Industrial metal bonding ultimately gets by with just a handful of adhesive types. Joining plastics to one another, or plastics to metals, requires suitable adhesives developed specifically for the task. Often, only a trial under real operating conditions can show whether a plastic adhesive will create a reliable bond. The reason is the enormous chemical diversity of plastics, which gives them widely varying physicochemical surface properties.
The Fundamentals of Adhesive Bonding
A secure, durable bond between two materials starts with understanding what happens during the bonding process.
Adhesive Forces Play a Key Role in the Bonding Process
First, the adhesive must wet the substrate surface thoroughly and adhere to it. These bonding forces, known as adhesive forces, arise from physical interactions between the substrate surface layer and the adhesive. They include polar interactions between polar groups, hydrogen bonds and non-polar dispersion forces, a type of van der Waals force.
For a strong, reliable bond, the adhesive and the plastic should match in polarity: both polar or both non-polar. Good wetting matters because adhesive forces act over a very short range of less than one nanometre. For plastics, surface energy describes how easily a surface can be wetted. Plastics with a higher surface energy, such as polyvinyl chloride (PVC), are generally easier to wet. Low-energy surfaces, such as those of polypropylene (PP), polytetrafluoroethylene (PTFE) and polyethylene (PE), resist wetting.
Cohesive Forces Hold the Adhesive Together
 Alongside the bond between the two surfaces, the adhesive also needs internal strength, which cohesive forces provide. These are the forces that act between atoms or molecules within a substance. During curing, cohesive forces govern parameters such as the viscosity and flow behaviour of the adhesive. They also determine the properties of the cured adhesive, including its tensile strength, temperature resistance and Shore hardness.
Key Factors for a Reliable Bonding Process
Careful planning from start to finish pays off, because many poor bonds stem from application errors. Consider the following points before bonding:
Designing the Components
Bonding plastics successfully requires parts that are designed “for bonding”. For example, the design must allow the adhesive to wet the contact surfaces completely. Engineers should also maximise the contact area between the parts. A bonded joint usually has to withstand external forces such as tensile or compressive loads, which can create stresses. The aim is to distribute these stresses as evenly as possible and avoid point loads. In addition, the plastic must not contain plasticisers. They can hinder bonding from the outset or escape over time and gradually weaken the bond.
Surface Pretreatment Is Essential
Treating the surface before the actual bonding is one of the most important steps. Dirt particles on the surface can impair wetting and with it the entire bonding process. Thoroughly removing adhering dust is therefore the first step towards a strong bond. Bonding plastics also requires removing oils, lubricants and other release agents. These can originate in the manufacturing process of the plastic, for example.
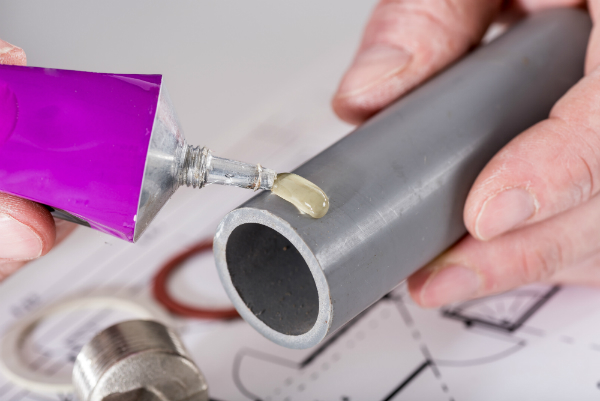
Low-boiling organic solvents such as acetone or alcohols work well for degreasing because they flash off easily. Plasma treatment, corona treatment and flame treatment rank among the most effective methods and therefore see the widest use. They also pose far fewer occupational health risks than handling solvents, and they prepare surfaces optimally for bonding. Another form of surface treatment uses primers or adhesion promoters. Applied immediately before bonding, they form a bridge between the plastic surface and the plastic adhesive.
Chemically active primers, by contrast, modify the surface structure so that plastic adhesives can wet it completely. Finally, mechanical roughening enlarges the surface area and so improves adhesion.
Requirements That Plastic Adhesives Must Meet
The type of plastic, its wettability and its surface energy determine which plastic adhesive is suitable. Further requirements for an adhesive for plastics depend on the application. The key question is how well the bonded joint resists temperature and humidity, as well as solvents and chemicals. Depending on the intended use, the adhesive must also meet physical criteria such as hardness, mechanical load resistance and elasticity.
Speciality adhesives offer particular properties – for example, plastic adhesives that become electrically conductive through added graphite or metal powders.
Different Types of Adhesives for Every Plastic
Plastic adhesives fall into two groups, depending on how they set: physically setting and chemically curing adhesives.
Physically Setting Adhesives
In physically setting adhesives, the polymer already exists in its final form, typically dissolved, dispersed or melted. They wet the surface well and solidify during the bonding process. In solvent-based wet adhesives, the solvent evaporates during bonding and the adhesive solidifies. Contact adhesives also belong to this group. So do pressure-sensitive adhesives. These carry a permanently tacky layer on a backing, as found on adhesive tapes or self-adhesive stamps. Hot-melt adhesives, which solidify again as they cool, are another physically setting type. They contain no solvents and allow thicker bond lines than many other adhesives.
Chemically Curing Adhesives
Chemically curing adhesives form the bond through a chemical reaction. This group divides into one-component and two-component adhesives. A typical example of one-component adhesives is cyanoacrylate adhesive, commonly known as superglue. Manufacturers often thicken the low-viscosity adhesive with fillers to make it easier to handle. With this type of adhesive, external conditions such as atmospheric moisture or UV light trigger the polymerisation. Silicone rubber adhesives crosslink on the same principle. Here, a liquid or paste-like silicone formulation crosslinks at room temperature. In construction, silicone rubber adhesive often serves as a sealant for joints.
Difficult Cases and the Right Plastic Adhesives
Acrylate-based adhesives for plastics, such as cyanoacrylates, bond many plastics. These include acrylonitrile butadiene styrene copolymer (ABS), polymethyl methacrylate (Plexiglas®, PMMA) and polycarbonate (PC). A modified adhesive based on methyl methacrylate (MMA) suits polyvinyl chloride (PVC), especially rigid PVC. These plastic adhesives can also bond polyolefins such as polyethylene (PE) and polypropylene (PP). This requires mechanically roughening the bonding surfaces or pretreating them with a primer first. However, such bonds do not always prove durable.
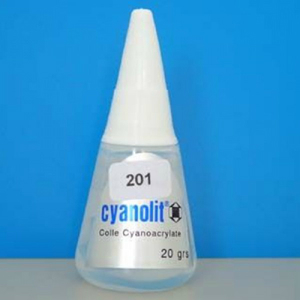
Bonding polytetrafluoroethylene (PTFE) and other fluoroplastics is particularly tricky. It requires pretreatment with special primers that chemically modify the bonding surfaces and so make them wettable. Manufacturers use stabilised solutions containing metallic sodium for this.
The free alkali metal in these formulations reacts with the chemically bound fluorine in the plastic. This leaves a roughened surface with a firmly adhering carbon layer that the adhesive can wet. Suppliers usually offer PTFE adhesives only in proven primer/adhesive sets to ensure the final joint holds.